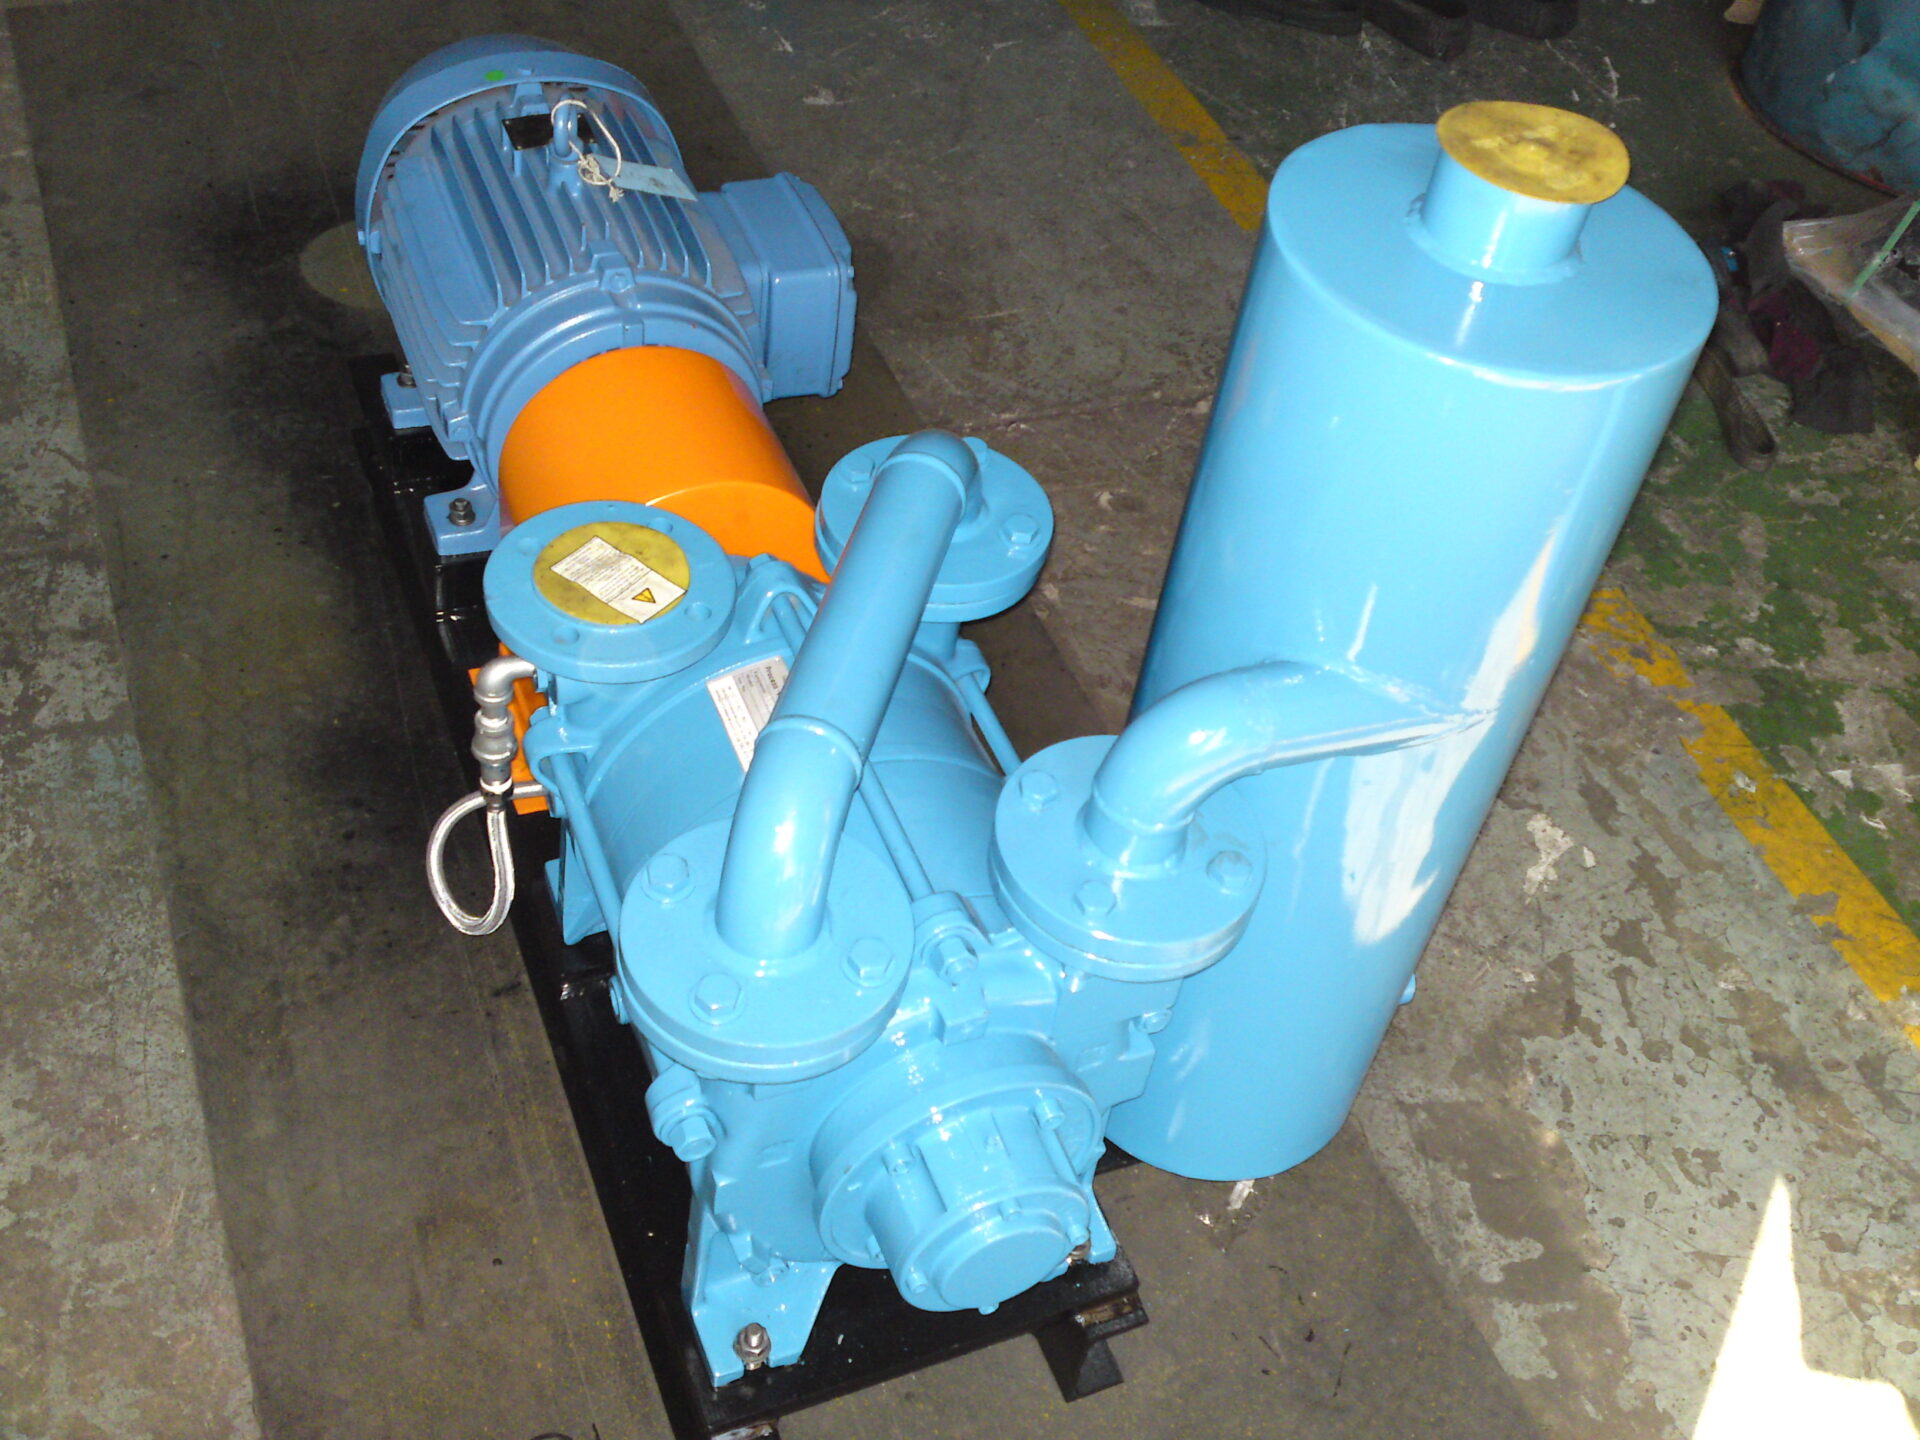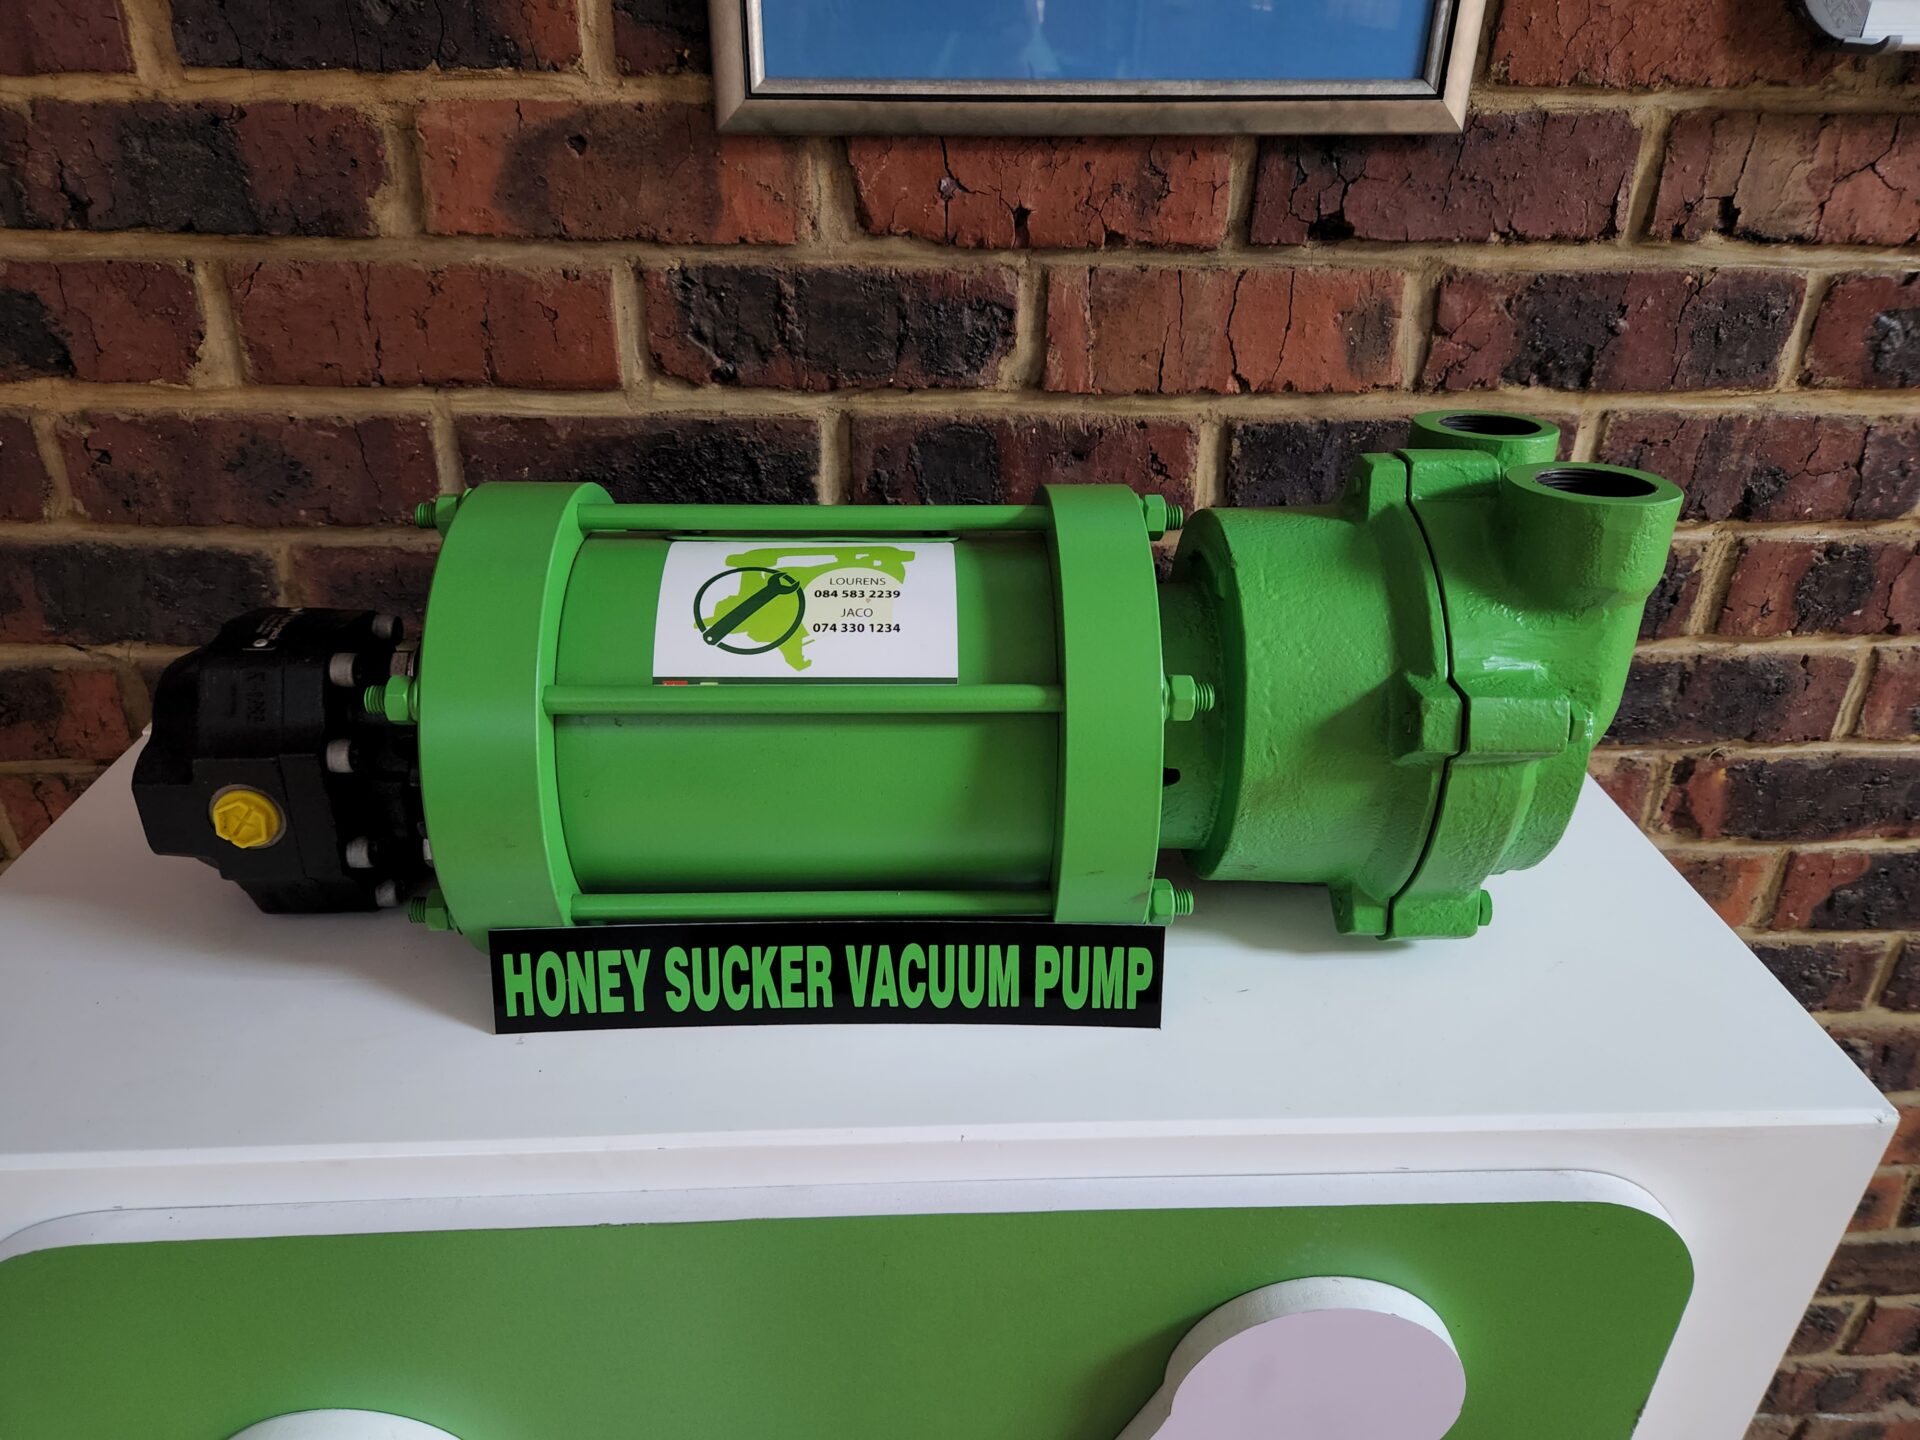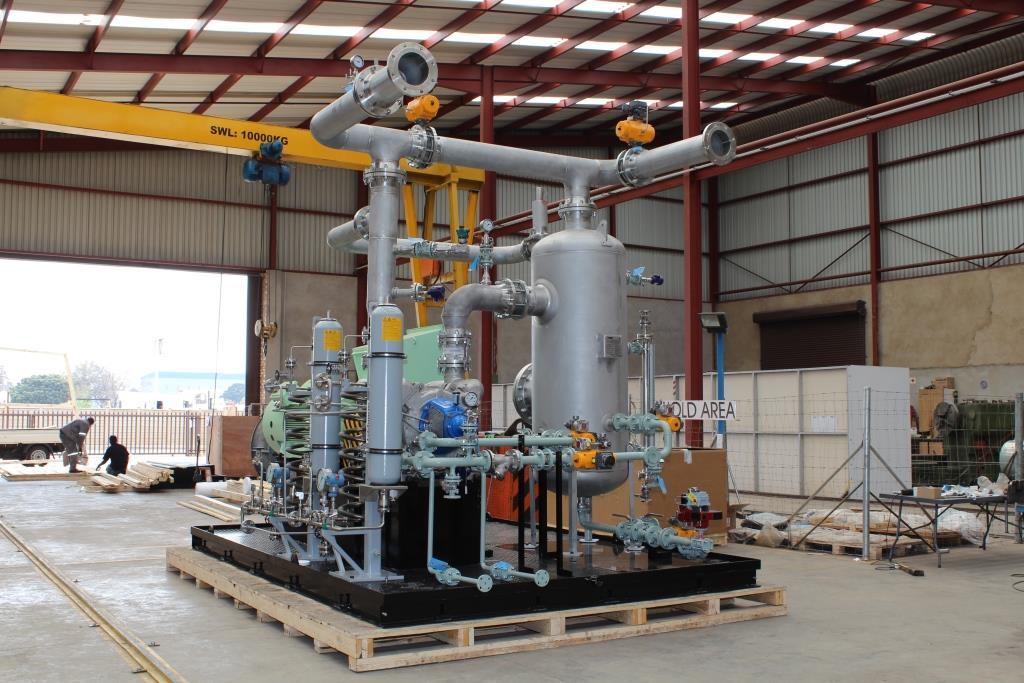
Chemical Dry Pumps are versatile and suited to a variety of chemical applications in the chemical, petrochemical and pharmaceutical industries. Chemical Dry Pumps provide a consistent vacuum at high efficiencies at a lower cost of ownership. At full vacuum Chemical Dry Pumps are very energy efficient. These pumps completely eliminate all possible contamination and creation of polluted effluents, which can be found in traditional wet vacuum pump technologies.
How it works
Dry pumps operate with two interlocking rotors that are situated on two parallel shafts. These shafts are synchronised by timing gears and rotate in opposite directions to trap and transport gases. There are three main types of dry vacuum pumps; rotary claw, rotary lobe and rotary screw pumps.
Applications of Chemical Dry Pumps
Chemical Dry Pumps are ideally suited for a wide range of applications in the above mentioned industries, including, but not limited to:
- Drying
- Distillation
- Evaporations
- Biofuels
- Corrosive gases
- Flammable gases
- Absorption
- Crystallisation
- Filtration
Features of Chemical Dry Pumps
Chemical Dry Pumps are designed for a life expectancy of no less than 25 years with very easy maintenance. These pumps can function for 12 months at a time with unattended operation and require 3 years between services. It is very cost effective to replace rotating parts, bearing cartridges are easily accessible and the pump is designed with the minimum number of bearings and seals possible to reduce wear.